In this deep dive
Soft enamel leaves the metal lines standing proud; hard enamel grinds them flush and polishes the surface flat. Neither is the better material. Soft enamel is the more forgiving surface for line-heavy artwork and the cheaper one to produce. Hard enamel is the more expensive, more uniform surface — the one that reads as a finished object rather than a printed badge. The decision usually turns on a single question: is this piece handled in bulk, or sold one at a time?
Terminology
Two names, one confusing vocabulary
Both names start from the same object: a metal body with recessed cells, formed by a stamping die or a die-cast mould. The cells are the artwork. Everything that separates the two methods happens after the color goes in.
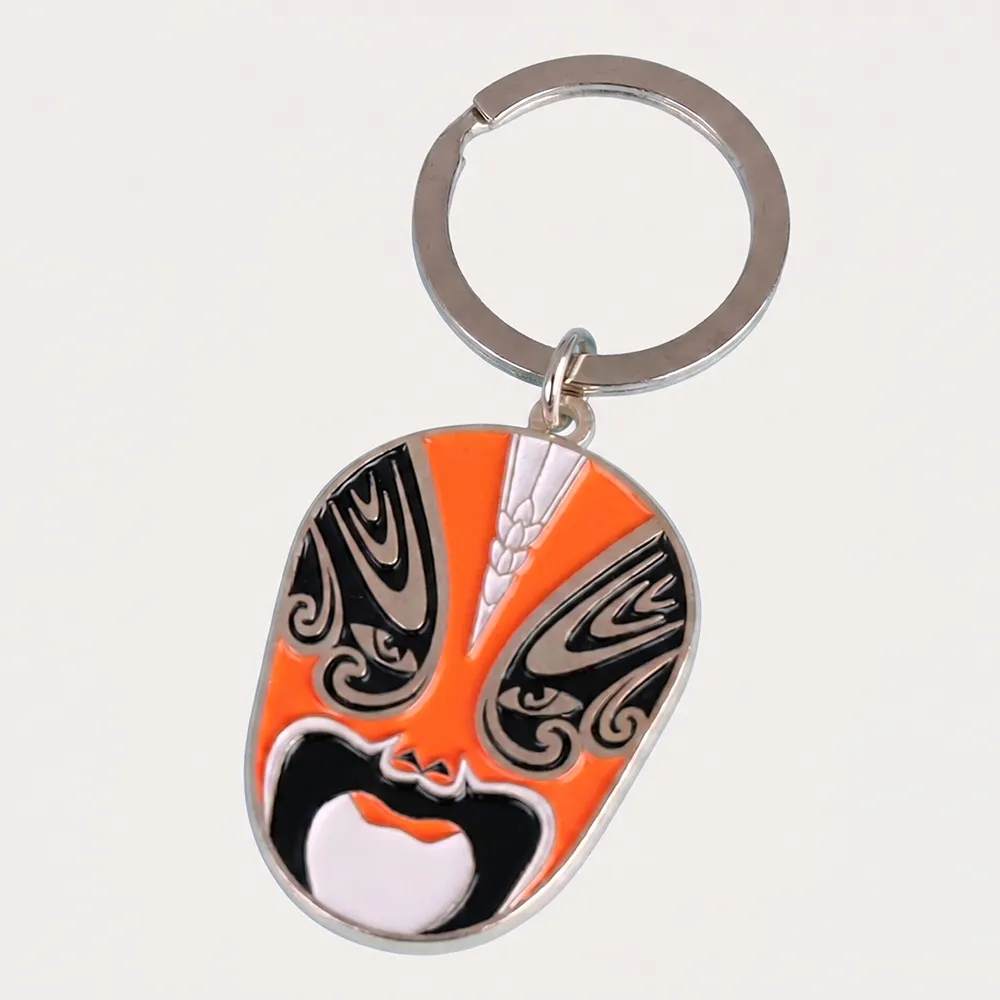
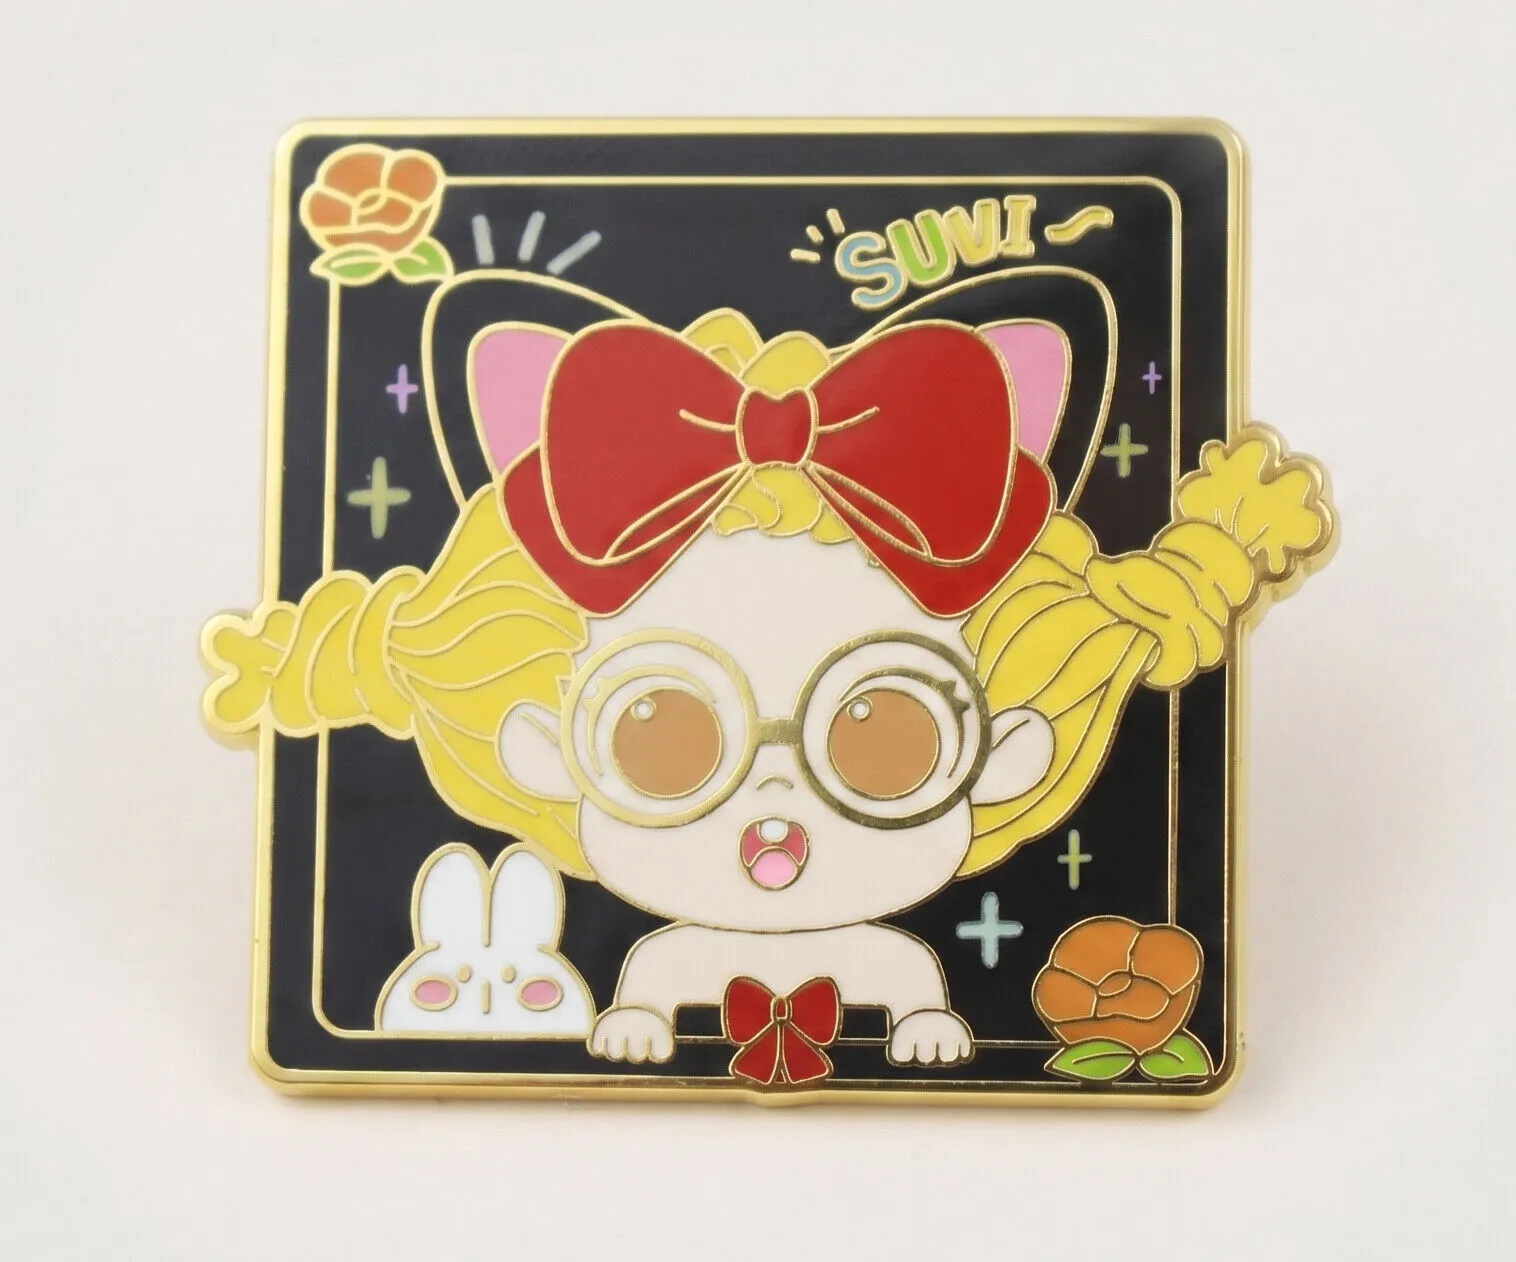
Soft enamel — 烤漆 in most Chinese supply chains — is filled and cured, and that is the end of the surface work. Hard enamel, 仿珐琅, is filled, baked, ground flat against the metal lines, polished, and then plated. The word “hard” describes the geometry of the finished face, not the hardness of the enamel itself: a cured soft enamel layer is hard too. What changes is that one surface has relief and the other does not.
仿珐琅 translates literally as “imitation cloisonné”, and that is the honest description. True cloisonné builds walls from wire, fills them with glass frit, and fires the piece repeatedly at high temperature before polishing it with stone. Imitation hard enamel reproduces the look with stamped metal walls and synthetic enamel. At arm's length the two are close. In durability, in labour, and in price, they are not the same craft — so a quotation that says “cloisonné” should be read as “hard enamel” until the process is confirmed.
Three questions that replace the label
- Is the color flush with the metal lines?
- Was the face ground and polished after filling?
- Was the piece plated after polishing?
Three yes answers mean hard enamel, whatever the quotation calls it. A no on any of them means you are buying a polished front on a soft enamel part.
Process
The cross-section explains the rest
A pin body is usually 1.5–3.0 mm thick, with cells cut 0.3–0.5 mm deep. The metal left standing between the cells is the line work you see in the artwork — usually 0.25–0.4 mm wide at the die. That ridge is the whole story.
In soft enamel, the color is deposited into the cells and cured. Surface tension and cure shrinkage pull the fill slightly below the crest, leaving a recess of roughly 0.05–0.15 mm. The piece is then plated, and the plating follows the relief — which is why the lines stay bright and the color stays in shadow.
In hard enamel, the cells are overfilled and baked, then the entire face is ground down on a wet abrasive belt until the metal crest is exposed. The surface is polished with compound, and the piece is plated afterwards — because grinding cuts through the first plating layer. Some shops plate before grinding as well, so the metal does not oxidise while it is being worked.
Because grinding removes material, a hard enamel body needs enough wall thickness and enough fill depth to survive it. The finished piece is usually a little heavier, and the metal lines are a little thinner at the crest than they were on the die. Every consequence on this page — how it feels, which artwork survives, how it wears, what it costs — comes from that one extra operation.
Perception
What you see and what you feel
Tilt a soft enamel piece under a desk lamp and every metal line throws its own thin shadow. The artwork reads as carved, because the surface is genuinely carved. Hard enamel under the same lamp returns one continuous reflection: the metal lines read as drawn lines, not as walls, and the design becomes a set of color fields bounded by hairlines.
In the hand the difference is just as literal. Soft enamel feels like letterpress — a fine series of ridges you can trace with a fingernail. Hard enamel feels like a glass tile: one plane, no texture, slightly cooler and denser.
Color behaves differently too, and this is where most approvals go wrong. A matte soft enamel field scatters light, so a Pantone match reads lighter and flatter on the finished pin than on the chip. A polished hard enamel field reflects its surroundings, so the color reads deeper and more even — and in product photography it will pick up whatever is in front of it. Judge both on the finished surface under D65, never on a screen.
| Surface | Under light | Color | How it ages |
|---|---|---|---|
| Soft, matte | Scatters light; every metal edge casts a fine shadow | Reads lighter and flatter than the chip | Dust settles into the wells and dulls the color |
| Soft, gloss | Brighter highlights, but the ridges still break the surface | Slightly deeper than matte, still not uniform | Shows handling marks on the high points |
| Soft + epoxy dome | One continuous glassy reflection | Rich and even at arm's length | Dome can yellow and micro-scratch; not a ground surface |
| Hard, polished | Reflects the room as one plane; lines read as drawn, not raised | Reads deeper and more uniform, and picks up surroundings in photos | Fine scratches appear on dark fields; wipes clean |
There is a third option that buyers often discover too late. A soft enamel piece can be finished with an epoxy dome: a resin layer that fills the recesses and levels the face. It looks close to hard enamel at arm's length and costs far less, but it is a coating, not a ground surface. Domes yellow under UV, scratch with handling, and soften fine type — they suit printed artwork better than line art.
Artwork
Where the artwork breaks
Both methods share the same hard limit: the design has to exist as closed cells of solid color separated by metal. What differs is how much of that design survives the finishing step. The numbers below are typical shop ranges rather than standards — treat them as the point where you should ask, not as a rule.
| Constraint | Soft | Hard | Why |
|---|---|---|---|
| Minimum metal line | ≈ 0.2 mm | ≈ 0.3 mm | Polishing rounds the crest, so a thin line loses its edge before it loses its width. |
| Smallest isolated color area | ≈ 0.3 mm across | ≈ 0.4 mm across | Surface tension pulls enamel out of tiny cells; grinding then opens the void. |
| Reversed-out text (metal letters) | ≥ 1.2 mm stroke | ≥ 1.5 mm stroke | Grinding removes the top of thin strokes; serifs soften first. |
| Gradients and halftones | Not in enamel | Not in enamel | Enamel is a solid color in a cell. Gradients need print, with or without a dome. |
| Two-level relief | Possible | Not possible | Grinding levels every height to one plane by definition. |
| Large uninterrupted color fields | Forgiving | Dishing risk | Holding a wide area perfectly flat through polishing is harder than filling it. |
| Color count | Rises with each color | Rises faster | Every added color is another pass that has to be re-levelled against the rest. |
The constraint that surprises most buyers is text. Reversed-out lettering — metal letters inside a color field — depends on a metal stroke surviving the finish. In soft enamel a 1.2 mm stroke is comfortable. In hard enamel the same stroke is ground and polished from the top down, so the letter loses weight and any serif detail softens into a suggestion. If the design depends on small type, it is a soft enamel design, and forcing it into hard enamel produces a pin that looks like a bad print.
Gradients and halftones are a separate problem: neither method can hold them, because enamel is a solid color in a cell. Those designs belong to offset or UV printing, with or without a dome. A halftone can be simulated with a grid of tiny cells, but the cells have a minimum size, so the dot pattern becomes visible and the cost climbs with every separation.
The working rule: if the design depends on thin lines, texture and layered relief, it was drawn for soft enamel. If it depends on silhouette, color blocking and a clean edge, it was drawn for hard enamel. Redrawing artwork for the wrong process costs more than the price difference between the two.
Durability
What actually fails first
“More durable” is the phrase most often used to sell hard enamel, and it is only half true. The two surfaces fail in different places, at different moments, for different reasons. Which one lasts longer depends on how the piece is used, not on which process is nominally superior.
One honest caveat before the detail: there is no industry-wide abrasion standard for decorative enamel fill. Durability claims about enamel are comparative, not certified. Plating is the part that can be tested — salt spray, abrasion cycles, nickel release — so when a supplier talks about durability, ask which test the number comes from.
Abrasion on the color surface
The color sits below the ridge line, so the metal takes most of the rubbing. The enamel survives contact but collects dust in the wells, and the color goes dull rather than worn.
The flat face takes abrasion directly. It resists scratching better than a paint layer, but on dark colors every fine scratch shows, and the surface holds fingerprints.
Impact and edge chipping
The raised ridge absorbs the hit first, so damage usually appears as a bright metal nick on a line rather than a missing patch of color.
Impact reaches color and metal at the same moment. A chip at the rim is more visible because there is no recess left to hide it.
Plating wear
The highest point is the metal line. Plating thins there first, so the line art slowly changes tone before the color does.
The highest point is the whole face. Plating wears evenly across it and reveals base metal as a patch rather than along a line.
UV and chemical exposure
Paint layers chalk and shift under long UV exposure; reds and blues move first.
The baked layer is more stable, but not immune. Chlorine, sunscreen and perfume attack the plating long before they reach the enamel.
The practical reading: soft enamel protects its color by putting metal in the way, so it survives knocks and bulk handling well and dulls gradually. Hard enamel protects itself with a denser, flatter surface, so it resists abrasion and cleans up well, but it shows scratches and edge chips more openly. A hard enamel pin with thin plating will still fail at the plating, exactly like a soft enamel one.
Durability is a system
Enamel method, plating thickness, attachment, and packaging determine survival together. Care is the same for both: dry microfibre cloth, no ultrasonic bath, no solvent, no stacking loose pins in a bag.
Cost
Where the price difference comes from
The tooling is the same. Both methods run off the same die or the same mould, so the mould fee does not change — that is a separate conversation, covered indeep dive 02. The difference is entirely in what happens to each piece after the color goes in.
- Labor
Extra fill passes
Grinding removes material, so the cells have to be overfilled and topped up between cures. Two or three passes instead of one.
- Labor
Grinding and polishing
Every piece is levelled against a wet abrasive belt and then polished. This is hand-fed work, and it is the single largest line in the difference.
- Material
Re-plating after grinding
Grinding cuts through the first plating layer. The piece is plated again afterwards, and sometimes polished once more.
- Yield
Higher reject rate
Pits, uneven grinding, chipped rims and color pulled across a line are all discovered after the expensive step, not before it.
- Time
Longer production window
More passes, more handling, more inspection points. The lead time moves out by days, not hours.
In practice, hard enamel usually prices 15–35% above soft enamel at the unit level, for the same design and quantity. The low end of that range belongs to simple shapes with few colors at volume; the high end belongs to multi-color designs with large flat fields, where grinding and polishing have more surface to keep level and the reject rate climbs.
The gap is labour-dominated, which means it does not behave like a material cost. Doubling the order does not halve the difference: the absolute gap per piece stays roughly flat, so the percentage narrows slowly while the money does not. If a quote shows hard enamel at soft enamel pricing, the more likely explanations are a polished front only, a domed print described as hard enamel, or a reject allowance quietly moved into the replacement terms.
There is also a cost that never appears on the enamel line. Hard enamel sets an expectation: a piece finished to that surface is usually presented on a backing card or in a box, and that packaging can cost more than the upgrade itself. Budget the presentation with the process, not after it.
Verification
How to verify it on a sample
None of the above matters if the goods arrive as something else. Five checks settle the question in under a minute, and none of them require a lab.
Rake the light
Hold the piece under a desk lamp at a low angle. Soft enamel throws a shadow along every metal edge. Hard enamel returns one continuous reflection across the face.
Drag a fingernail
Pull across a color field. Soft enamel catches on the ridges in a fine series of steps; hard enamel glides.
Look at the edge, not the face
A 10× loupe or a phone macro shot at the rim settles it. Soft enamel shows the color sitting below the metal edge; hard enamel meets it flush.
Check the reverse
Some suppliers polish the front only. If the back and the recesses around the attachment are still rough, the piece was not processed as a hard enamel part.
Write the process into the PO
Specify “color flush with the metal lines, surface ground and polished, plated after polishing”. The words “hard enamel” alone are a label, not a specification.
One last distinction worth making explicit in the order: a golden sample from the tooling shop and a production sample from the running batch are not the same object. Ask for the second one before the bulk run, and keep the approved piece sealed as the reference for the inspection.